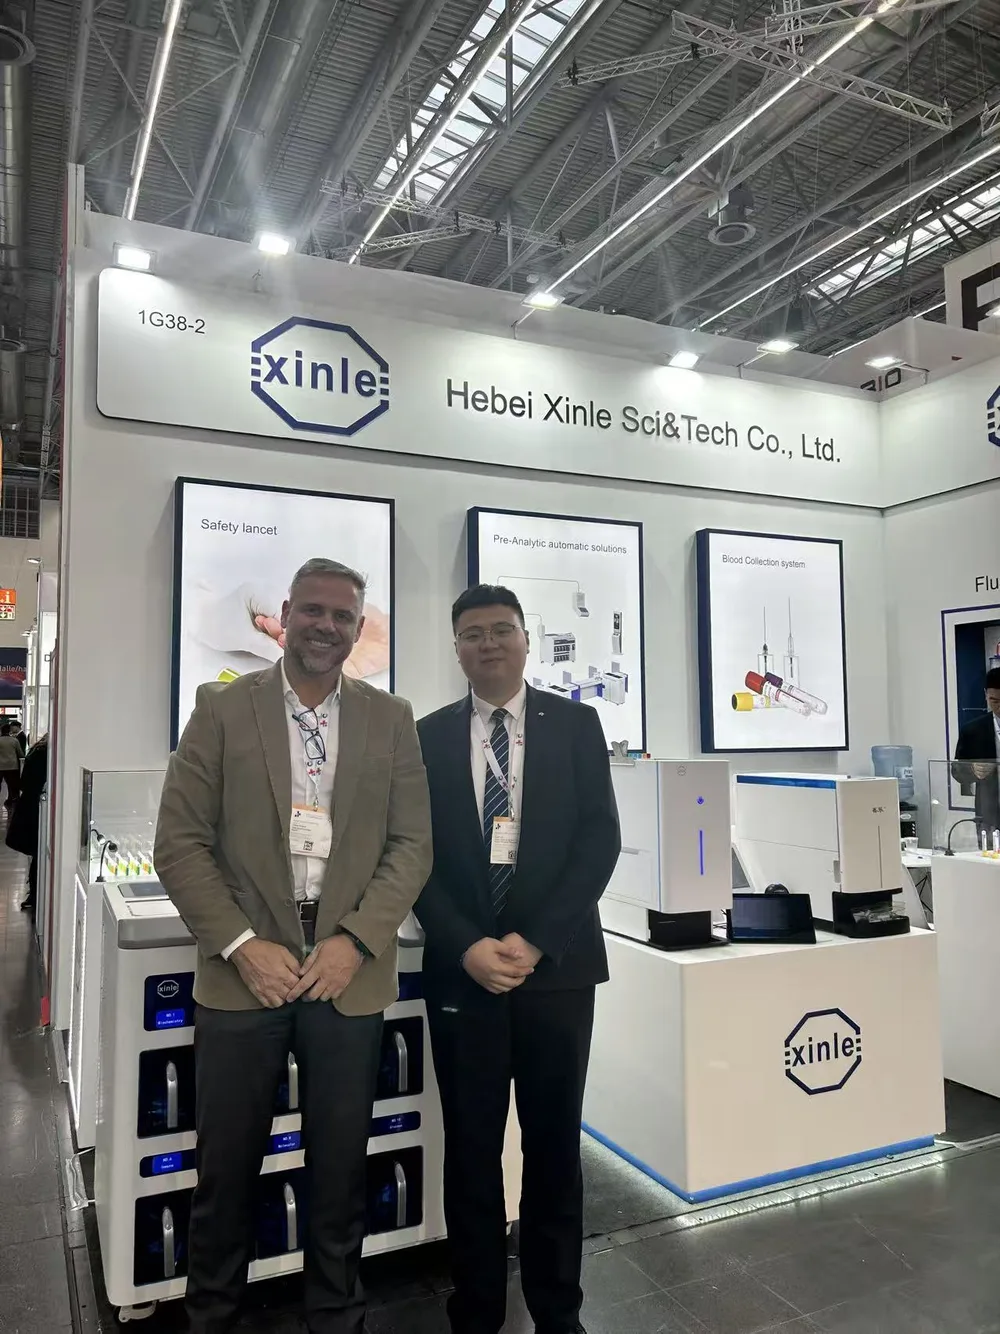
At Xinle Medical, every product begins with the same question: how can we make the clinical workflow safer, faster and more dependable? From blood collection consumables to intelligent pre-analytic automation, our engineering teams focus on the steps where accuracy and traceability matter most.
Engineering for Reliability
Reliability in the laboratory is not a single feature — it is the product of disciplined design, rigorous validation and consistent manufacturing. Each system we ship is tested against the demanding conditions of high-throughput clinical environments, where a single labeling or sorting error can ripple across an entire batch.
Quality is not inspected into a product after it is built; it is designed in from the first sketch and verified at every stage.
Built on a Foundation of Standards
Our quality management system is certified to ISO 13485, and our products carry CE marking alongside other international approvals. This commitment means that the same controls govern a single blood collection tube and a full laboratory automation line.
Looking Ahead
As laboratories adopt more connected, data-driven workflows, Xinle Medical continues to invest in R&D that closes the gaps between collection, transport, sorting and analysis. Our global sales network now spans more than 70 countries and regions, supported by local service teams and rapid technical response.
- End-to-end pre-analytic automation for clinical laboratories
- Pharmacy dispensing and PIVAS drug management solutions
- Full batch traceability and LIS / HIS integration